
In the fiercely contested world of ultra-premium wines and rare spirits, packaging aesthetics represent the immediate physical embodiment of a brand’s pedigree. Discerning consumers and seasoned collectors assess bottle presentation with uncompromising scrutiny, evaluating everything from glass weight to label typography. Yet, among all exterior components, the tamper-evident capsule—often called the secondary closure—serves as the primary tactile threshold between the consumer and the liquid inside.
Beyond aesthetic distinction, capsules provide an essential barrier that safeguards wine integrity during multi-year cellaring and international transit. However, executing flawless capsule finishes at commercial bottling speeds presents profound mechanical obstacles. While material selection dictates the initial tactile quality of the closure, consistent wall thickness and flawless skirt crimping depend entirely on the mechanical tolerances of secondary converting machinery.
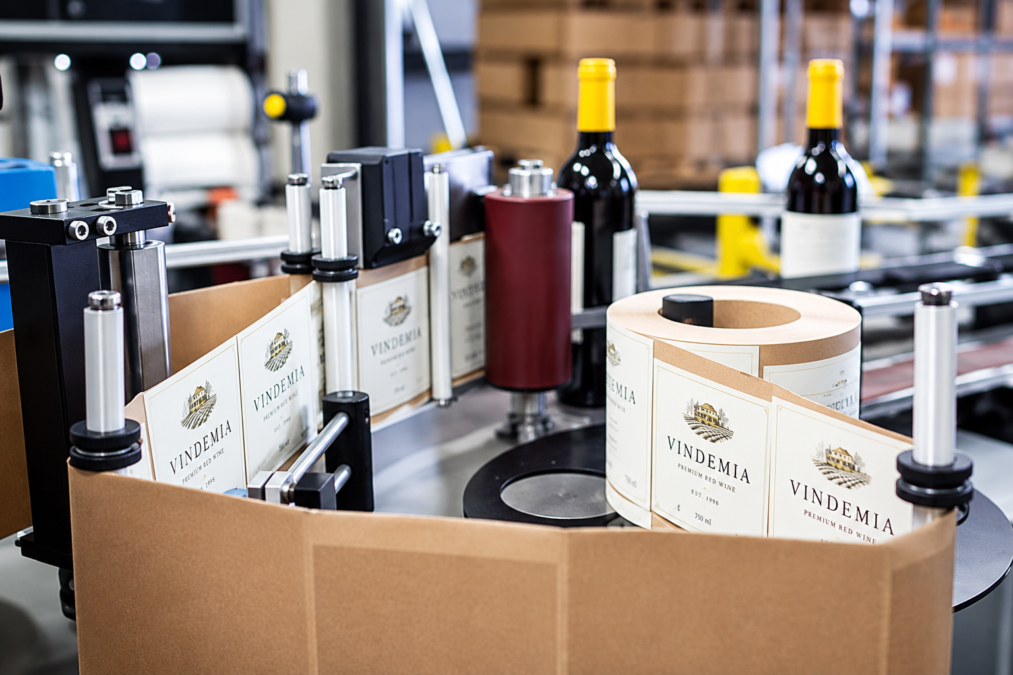
Equipment engineers at KETE have demonstrated that high-precision wine capsule machines—capable of handling both PVC heat-shrink films and complex polylaminate composites—must maintain registration accuracy within fractions of a millimeter during automated top-disc punching and skirt heat-sealing, preventing aesthetic wrinkling across high-speed bottling lines.
The Dual Role of Wine Capsules: Brand Storytelling Meets Tamper Evidence
Secondary closures historically functioned as simple utilitarian barriers designed to deter rodents and insect infestation in subterranean cellars. In contemporary luxury merchandising, their functional mandate has evolved into a sophisticated synthesis of anti-counterfeiting security and brand narrative.
Luxury Brand Perception at the Point of Uncorking
The tactile sequence of uncorking a vintage wine or reserve single malt Scotch establishes an intimate psychological connection with the consumer:
- Tactile Ceremony and Elegance: The physical resistance, structural rigidity, and smooth cut of the capsule under a sommelier’s knife signal authenticity and premium craft.
- Preventing Atmospheric Infiltration: A properly seated capsule shields the porous natural cork from ambient micro-contaminants, ultraviolet exposure, and external moisture fluctuations.
- Tamper-Evident Deterrence: Counterfeiting cartels frequently target empty vintage bottles by refilling them with inferior liquid. Precision-engineered capsules with proprietary tear lines and micro-perforations cannot be extracted intact, creating an irreversible visual break that deters illicit re-corking.
When capsules suffer from mechanical crimping defects, uneven pleats, or distorted brand crests, consumer trust degrades immediately, undermining the price premium commanded by high-end vintages.
Material Evolution: PVC vs. Polylaminate vs. Pure Tin
The transition toward premium bottle presentation has prompted a rigorous technical re-evaluation of capsule substrates:
- Polyvinyl Chloride (PVC) and PET-G: Historically prized for rapid thermal contraction and low unit cost. However, thin shrink films exhibit a glossy, plasticized feel that clashes with luxury branding, while PVC faces progressive regulatory bans across Europe due to chlorine recycling contamination.
- Pure Spun Tin: Regarded as the undisputed pinnacle of luxury closures. Spun tin delivers a seamless, soft-metal hand-feel and accepts intricate blind embossing. Nevertheless, geopolitical commodity price spikes, heavy tare weight, and high manufacturing costs limit pure tin to ultra-luxury prestige cuvées.
- Polylaminate Composites (Al/PE/Al): Comprising a three-layer sandwich of aluminum, polyethylene, and aluminum, polylaminate has emerged as the definitive engineering compromise for luxury spirits. It combines the metallic drape and tactile heft of pure tin with the structural versatility of composite polymers, at a fraction of the raw material cost.
Technical Precision in Secondary Forming and Shrinking
Achieving flawless capsule application across high-speed packaging lines requires deep mechanical harmony between substrate physics and automated forming machinery.
Managing Heat Shrink Uniformity and Thermal Distortion
For thermal-shrink films such as PET-G, maintaining structural symmetry depends on thermodynamic equilibrium within the heating tunnel:
- Operating Thermal Windows: Heat-shrink tunnels and automated rotary heating heads must operate within strict thermal bands between 250°C and 320°C.
- Thermal Distortion Risks: Exposure to uneven airflow profiles or localized hot spots triggers asymmetric shrinkage. This pulls multi-color brand graphics out of square, creates lateral distortion, and results in unsightly “dog ears” along the bottle neck contour.
- Controlled Thermal Exposure: Converting lines mitigate this through rapid rotational bottle positioning and multi-stage laminar hot-air manifolds, ensuring balanced radial contraction within cycle windows measured in milliseconds.
C-Skirt Rolling and Top-Disc Piercing Technologies
Unlike heat-shrink polymers, metallic polylaminates do not contract under thermal exposure; they require mechanical crimping and automated rolling:
- Continuous Skirt Forming: High-speed capsule converting machinery punches circular top discs from coated foil coils while simultaneously forming the cylindrical body skirt from continuous web ribbons.
- Ultrasonic Spot Welding: Skirt side-seams are fused using precision ultrasonic horns or localized micro-hot-melt beads. The weld must remain utterly undetectable on the exterior face.
- Degassing Ventilation Holes: Natural corks release minute volumes of headspace gas during temperature shifts. Precision mechanical punch units integrate micro-venting needles into the top disc to vent pressure without allowing external contaminants to enter.
High-End Decoration: Top Embossing, Hot Foil Stamping, and Teartape Integration
Visual distinctiveness in luxury spirits requires multi-stage inline embellishment that challenges traditional toolmaking tolerances.
Micro-Embossing Registration on Aluminum Foils
Embossing brand heraldry and tactile crests onto thin metallic substrates requires extreme mechanical accuracy:
- Substrate Caliper Constraints: Luxury polylaminate capsules utilize aluminum foil plies with calipers between 0.08 mm and 0.12 mm.
- Rotary Tooling Tolerances: Hardened steel die tooling must strike the composite substrate with micro-metric depth calibration. Excessive impact pressure fractures the outer aluminum layer, exposing the translucent polyethylene core.
- Dynamic Registration: Modern converting equipment integrates computerized optical sensor tracking to synchronize hot-foil stamping and multi-level relief embossing within a registration tolerance of
 .
- Integrated Tear Tapes: To facilitate clean opening without jagged foil edges, converting lines apply self-adhesive tear strips or precision laser micro-perforations inline, ensuring effortless separation for the end consumer.
Key Takeaways
| Area | Key Takeaway | Impact/Data |
| Material | Adopt polylaminate composites to replace banned PVC. | Reduces costs vs pure tin; eliminates chlorine risks. |
| Precision | Enforce micro-metric tooling tolerances during stamping. | Registration within 0.15mm; prevents aluminum fracture. |
| Security | Integrate 2D serialization and tear tapes inline. | 100% automated anti-counterfeiting audit compliance. |
Global Standards and Traceability in High-Value Beverage Logistics
As high-value wines and spirits navigate international bonded warehouses and customs checkpoints, packaging components must demonstrate verifiable regulatory compliance.
Anti-Counterfeiting Integrity in International Spirits Distribution
For international export validation, premium vintners must align their closure integrity with the regulatory guidelines compiled by the International Organisation of Vine and Wine, which dictates strict thresholds for head-space inert gas retention, migration limits for contact materials, and standardized capsule removal geometries for consumer safety.
Global brand protection frameworks mandate that converting lines incorporate machine-readable security features:
- Covert Digital Serialization: Modern capsule lines integrate high-resolution continuous inkjet (CIJ) or UV-laser marking engines to print unique 2D DataMatrix codes directly onto the inner skirt or underside of the top disc.
- Optically Variable Inks (OVI): Converting machinery applies color-shifting taggants and luminescent pigments that react to specific forensic light wavelengths during customs inspections.
- Mechanical Integrity Audits: High-speed automated vision systems inspect 100% of finished capsules on the delivery starwheel, immediately rejecting units with microscopic skirt cracks, misaligned tear tapes, or distorted embossing before shipment to commercial bottling facilities.